THERMOFORMING PROCESS EXPERTISE

Independent Thermoforming Expertise.

From Extrusion to the Final Part.

Troubleshooting, process optimization and training for thin gauge, heavy gauge and sheet extrusion operations worldwide.

THERMOFORMING PROCESS EXPERTISE

Independent Thermoforming Expertise.

From Extrusion to the Final Part.

Troubleshooting, process optimization and training for thin gauge, heavy gauge and sheet extrusion operations worldwide.

WHEN THERMOFORMING BECOMES TROUBLESHOOTING

The machine is running.
But the process isn't.

Quality issues. Process variation. High scrap. Long cycle times.
Problems that keep coming back — even after adjustments have been made.

01

QUALITY

Uneven wall thickness
Unstable sealing rims
Visual defects
Part variation

02

PRODUCTIVITY

Long cycle times
Low output
Unstable process speed
Constant parameter adjustments

03

SCRAP & COST

High scrap rates
Excess material usage
Frequent rejects
Recurring process problems

INDEPENDENT PROCESS SUPPORT

Fresh Eyes. Fast Impact.

I look at the complete thermoforming process — from extrusion and machine settings to tooling and the final part.

Independent of machine builders and toolmakers, I focus on one thing: finding the real cause behind the problem.

THE COMPLETE PROCESS

EXTRUSION

Material
Sheet quality

MACHINE

Process settings
Performance

TOOL

Forming process
Performance

PART

Quality
Process stability

MY APPROACH

From symptom to root cause.

Changing parameters can hide a problem.
I focus on understanding why the problem exists in the first place.

01

OBSERVE

Understand the process before changing it.
Machine. Tool. Material. Timing. Part.

02

MEASURE

Measure what actually happens.
Pressure. Temperature. Timing. Flow.

03

SOLVE

Correct the root cause — not just the symptom.
Stable process. Repeatable results.

REAL CASES

Problems I find in real production.

The symptom is often visible. The real cause is somewhere else.

01

SLOW FORM-AIR BUILD-UP

Good parts at lower speed. Quality problems at higher speed.

ROOT CAUSE

The required pressure was available — but the pressure build-up inside the cavity was too slow.

Air volume · Flow rate · Valves · Supply lines · Tool distribution

02

UNSTABLE PART WEIGHT

Part weight varied from cycle to cycle.

ROOT CAUSE

Prestretch started before the mold was fully closed — changing the amount of material available for each cycle.

Process sequence · Prestretch · Mold closing · Material

03

TOO MUCH MATERIAL IN THE BOTTOM

The bottom was too thick while material was missing in critical wall areas.

ROOT CAUSE

The plug geometry moved too much material into the bottom instead of distributing it into the sidewalls.

Plug geometry · Plug timing · Temperature · Material distribution

04

WAVY BOTTOMS AT HIGHER SPEED

Good parts at lower speed. Wavy bottoms appeared when production speed increased.

ROOT CAUSE

The parts did not have enough time to cool before leaving the mold.

Cooling · Mold temperature · Water flow · Cycle time

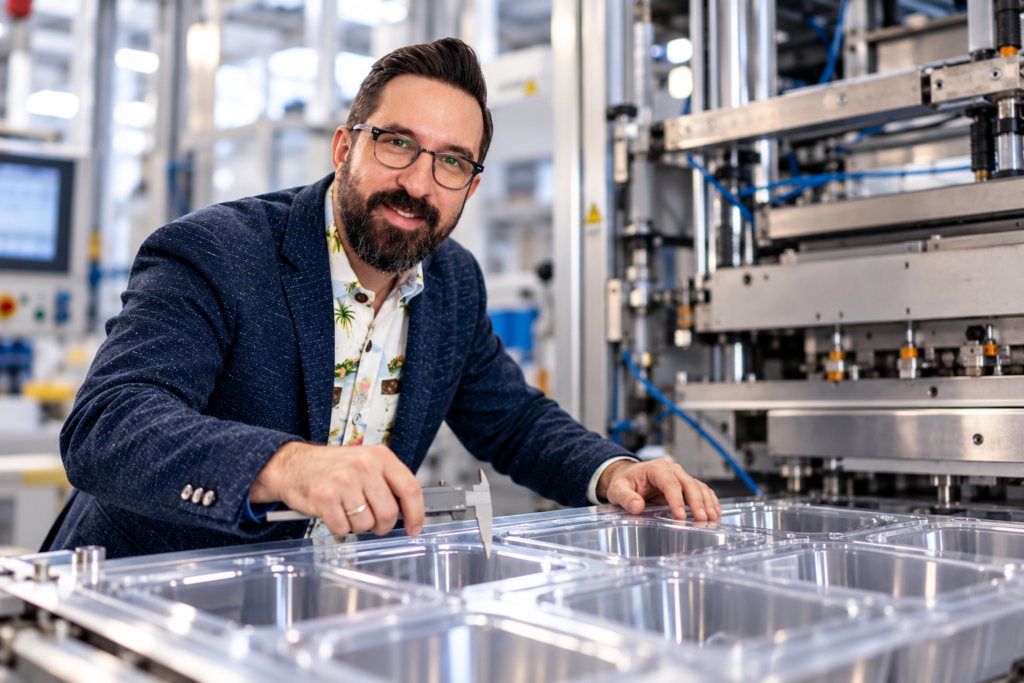
Thermoforming Consultant Andreas Dobringer

THERMOFORMING CONSULTANT · 30+ YEARS OF EXPERIENCE

Thermoforming experience. From production to problem solving.

30 years in thermoforming — from production and process development to working as an independent thermoforming consultant, troubleshooting processes around the world.

Different machines. Different tools. Different materials. Different problems. The goal has always been the same: stable quality and a repeatable process.

30+ YEARS

Hands-on thermoforming

WORLDWIDE

On-site process support

INDEPENDENT

Independent of machine and tool manufacturers

SEE THERMOFORMING IN ACTION

Sometimes you need to see the process to understand the problem.

Real machines. Real processes. Real production.

You are currently viewing a placeholder content from YouTube. To access the actual content, click the button below. Please note that doing so will share data with third-party providers.

More Information

ON SITE. WORLDWIDE.

Working with thermoforming teams around the world.

From troubleshooting and process optimization to training and production support — directly where the process happens.

CUSTOMER FEEDBACK

Trusted where results matter.

ELMES PACKAGING INC.

“The fastest way to master a new capability is to learn from someone who has spent a career perfecting it.”

“His guidance is helping us commission our new equipment to a high standard from day one.”

New forming line commissioning
Canada

GOINS PLASTIC Source

“If I had met you earlier, we would have saved a lot of time and money.”

Stacking optimization
Texarkana, USA

EVOLUPAK Plastic Inc.

“That was quick.”

Within just 15 minutes, one of the main process bottlenecks was identified.

Process troubleshooting
Canada

LET'S TALK

HAVE A THERMOFORMING CHALLENGE?

Tell me what is happening in your production. Let’s find out where the problem really starts.